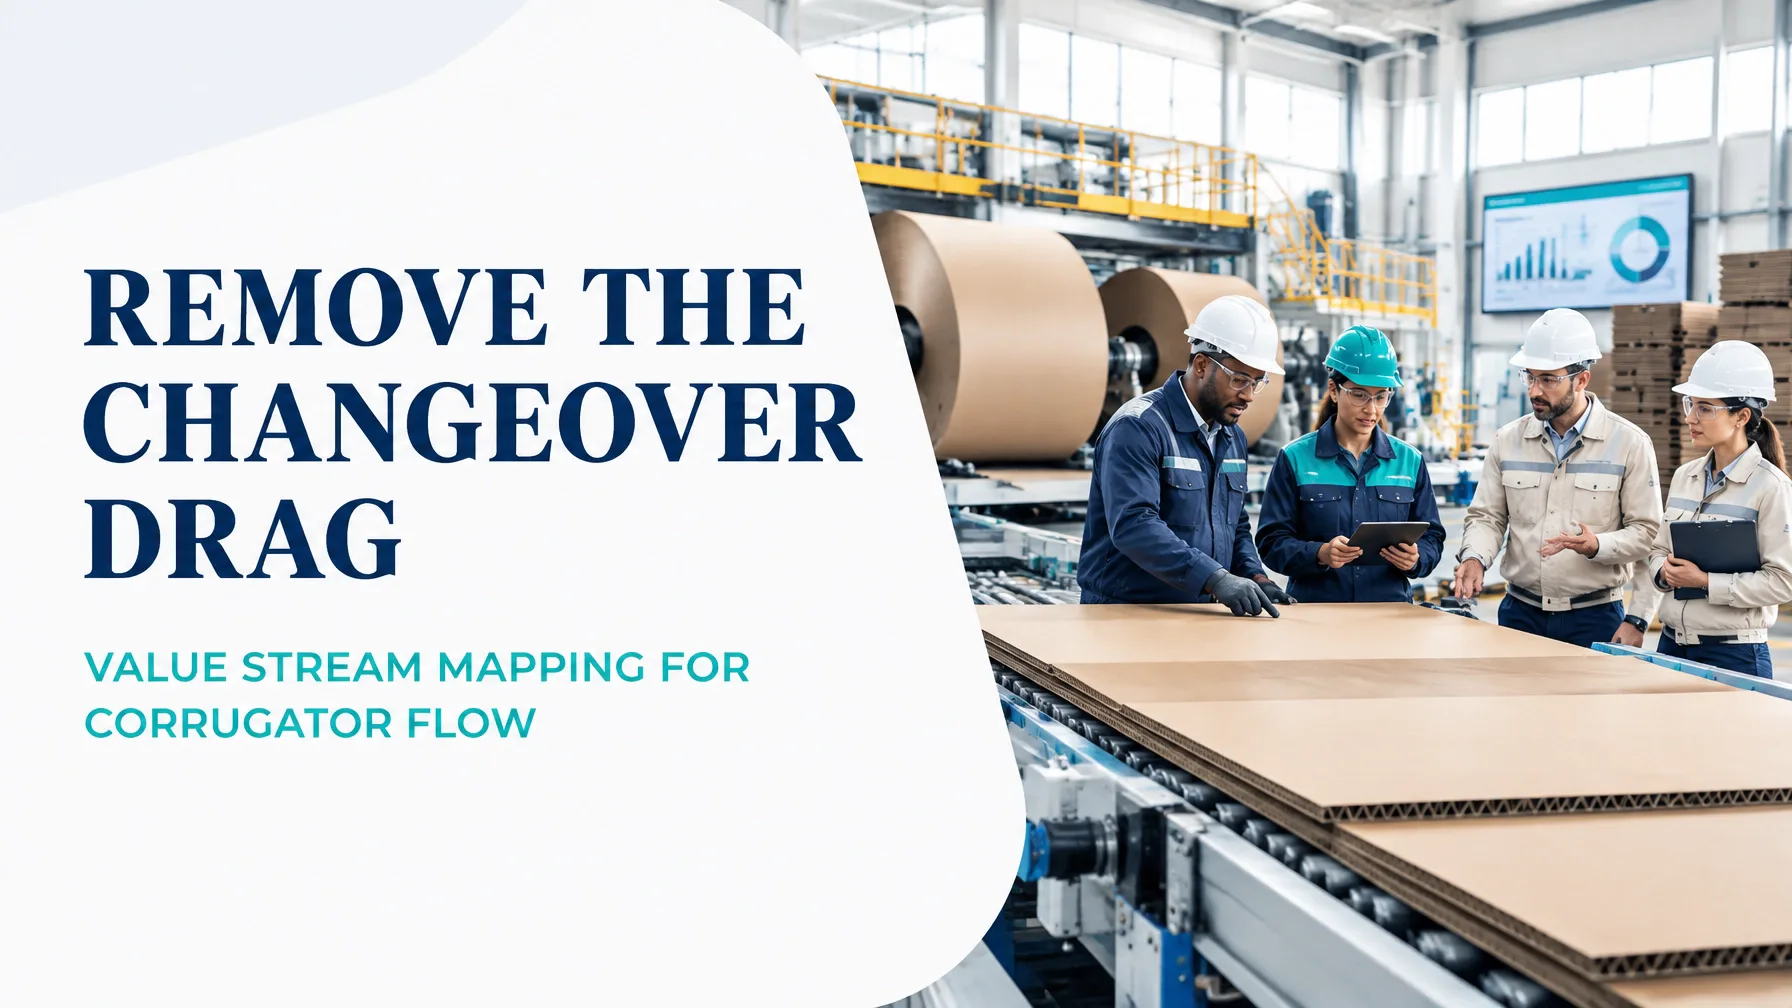
Corrugated board production can appear highly efficient from a distance: paper reels feed continuously into a corrugator, starch bonds the layers, and finished board exits in stacked bundles. Yet the value stream often tells a different story.
A sheet plant may have only 34 minutes of wet-end-to-bundling process time, while customer orders remain in the system for 6.2 days. The gap is created by changeovers, queues, excess work in process, quality holds, scheduling delays and material movement.
This guide applies Value Stream Mapping (VSM) to a corrugated board plant supplying box plants. The case study uses a two-shift, 2.4-metre corrugator operating at 180 metres per minute.
The production sequence follows the industry model described by the European Federation of Corrugated Board Manufacturers: reel paper is unwound, the medium is fluted in the single facer, starch is applied, the outer liner is bonded in the double backer, and the board is slit, cut and stacked.
1. Select the right VSM scope
The first decision is scope. Mapping every grade, flute, customer and downstream converting operation at once creates an attractive diagram but a weak improvement plan.
For this case, the product family is:
Standard single-wall corrugated board produced on the 2.4-metre corrugator and dispatched in bundled sheets to box plants.
The map begins at reel-paper release and ends at bundled board ready for dispatch. Information flow includes:
- Weekly customer orders in lineal metres
- Production scheduling and order sequencing
- Paper-reel availability
- Corrugator recipes
- Quality release and dispatch confirmation
The Voice of the Customer requires 97% DIFOT. The Voice of the Business requires higher OEE, lower trim and reduced working capital. The Voice of the Process is represented by actual run data: OEE, changeover duration, defect rate, WIP and throughput.
A cross-functional team should include planning, paper stores, corrugator operators, starch-kitchen personnel, maintenance, quality and dispatch. A Black Belt can facilitate the project, while Yellow Belts support data collection and daily experiments.
2. Current-state map with worked numbers
The current material flow is:
Paper reels → Reel stands and preheaters → Single facer → Bridge accumulation → Glue machine and double backer → Slitter scorer and cutoff → Bundling → Dispatch
The plant operates:
- Two shifts
- 2.4-metre machine
- 180 metres per minute rated speed
- 9 changeovers per shift
- 42 minutes average lost run time per changeover
- 61% OEE, against a 78% target
- 7.8% trim waste, against a 3.9% target
- 4.2% off-corrugator defects
- 2,900 tonnes of WIP
- 6.2-day order-to-dispatch lead time
- 34 minutes wet-end-to-bundling process time
- 91% DIFOT
Takt time calculation
Assume five operating days per week, two eight-hour shifts per day and weekly demand of 576,000 lineal metres.
Gross available time is:
5 days × 2 shifts × 8 hours × 60 minutes = 4,800 minutes per week
Therefore:
Takt time = 4,800 minutes ÷ 576,000 lineal metres
= 0.00833 minutes per lineal metre
= 0.5 seconds per lineal metre
This is equivalent to a customer demand rate of 120 lineal metres per minute, below the machine’s 180-metre-per-minute rated speed.
However, the changeover burden is substantial:
9 changeovers × 2 shifts × 5 days × 42 minutes
= 3,780 minutes of lost run time per week
Only 1,020 minutes remain from the nominal 4,800-minute schedule. To produce the assumed weekly demand in that remaining window, the corrugator would need to run at approximately 565 metres per minute, which is impossible.
The conclusion is direct: the plant cannot solve this problem by asking operators to run faster. It must reduce changeover frequency, shorten changeover duration and improve schedule stability.
The value-added ratio also reveals the scale of the opportunity:
34 minutes ÷ 8,928 total minutes in 6.2 days
= 0.38% process-cycle efficiency

3. The eight DOWNTIME wastes in the current state
The map should identify all eight Lean wastes, using plant evidence rather than assumptions.
- Defects: 4.2% off-corrugator defects are associated with starch viscosity and single-facer alignment. Typical symptoms include delamination, warp, loose flutes and edge issues.
- Overproduction: Long runs may be scheduled to keep the corrugator busy, creating board that is not immediately required by the box plant.
- Waiting: Board waits for the next operation, quality release, dispatch space, paper reels, maintenance support or approval.
- Non-utilised talent: Operators frequently compensate for unstable recipes and alignment conditions instead of contributing to structured root-cause analysis.
- Transportation: Reels, intermediate stacks and finished bundles may travel multiple times because storage locations and dispatch priorities are not synchronised.
- Inventory: 2,900 tonnes of WIP conceal schedule problems, consume space and extend lead time.
- Motion: Operators search for setup tools, gauges, recipes, inspection equipment and paper documentation during changeovers.
- Extra-processing: Re-inspection, re-bundling, sorting and repeated data entry consume capacity without increasing customer value.
An Affinity Diagram can group observations into changeover, quality, flow, planning and material-handling themes. A Time Observation Sheet should record actual setup tasks, queue duration and process time at the gemba.
4. Analyse the causes, not only the symptoms
The Analyse Phase should connect the losses to measurable inputs. In this case:
Y = f(x)
Board quality and delivery performance = f(starch viscosity, web alignment, speed, paper grade, deckle setting, recipe accuracy and schedule sequence)
Useful analysis methods include:
- Use an average and median for changeover duration, then display the spread in a box plot to expose long-tail events.
- Use attribute data, such as Pass/Fail bond checks, to stratify defects by paper grade, shift and operator.
- Apply ANOVA to compare mean changeover or defect results across shifts, flute profiles or product families. Bartlett’s Test can first assess whether group variances are sufficiently equal for the planned comparison.
- Use an X-bar and R chart for starch viscosity or alignment measurements to distinguish process shifts from routine variation.
- Use z-scores to identify unusually long changeovers or abnormal viscosity readings.
- Confirm measurement reliability. Instrument bias, poor sampling technique or inconsistent defect definitions can misdirect the project.
The plant should also install an Andon response for web breaks, bond failures, abnormal viscosity and alignment deviations. With autonomation (Jidoka), the process can detect a condition, alert the team and stop or contain the problem before a long run of defective board is produced.
The Theory of Constraints reinforces the same conclusion: identify the step limiting throughput, exploit it, subordinate other activities to it and improve it. Here, the corrugator’s effective capacity is constrained by changeover loss and unstable quality, not simply by rated speed.
5. Build the future-state map
The future state should be designed around flow, not isolated machine utilisation.
Future-state principles
- Establish the corrugator as the pacemaker process.
- Sequence orders by flute, paper grade and width where customer demand allows.
- Create a finite production schedule linked to weekly demand.
- Use SMED to separate external preparation from internal changeover work.
- Pre-stage reels, recipes, starch and setup tools before the machine stops.
- Standardise single-facer alignment checks and starch-viscosity verification.
- Introduce FIFO lanes between corrugation and bundling.
- Set WIP limits and escalate when the limit is reached.
- Use daily visual management for OEE, trim, defects, DIFOT and changeover time.
- Replace informal approval chains with clearly defined decision rights.
Formal approval checkpoints remain important for quality and governance, but unnecessary signatures can become bottlenecks. One accountable release owner and a defined escalation time are usually stronger than multiple sequential approvals.
Current versus future state
| Metric | Current state | Future-state target |
|---|---|---|
| Order-to-dispatch lead time | 6.2 days | 2.8 days |
| Wet-end-to-bundling process time | 34 minutes | 28 minutes proposed |
| Corrugator OEE | 61% | 78% |
| Average changeover duration | 42 minutes | 20 minutes proposed |
| Trim waste | 7.8% | 3.9% |
| Off-corrugator defect rate | 4.2% | 1.6% |
| WIP | 2,900 tonnes | 1,450 tonnes proposed control target |
| DIFOT | 91% | 97% |
| Customer-demand pace | 120 m/min gross takt | Sustain without changeover overload |
The proposed WIP and changeover targets are design assumptions for the future-state workshop and must be validated through pilot data. The specified targets (2.8-day lead time, 3.9% trim, 1.6% defects and 97% DIFOT) should remain the project’s primary CTQs.

6. A 30/60/90-day kaizen sequence
Days 1–30: Stabilise and see the work
- Confirm product-family scope and map the gemba process.
- Validate the measurement system for trim, defects, viscosity and alignment.
- Establish an Andon escalation standard.
- Create a changeover video and time-observation baseline.
- Separate internal and external setup tasks.
- Begin daily review of OEE, DIFOT, WIP and defects.
- Use an Agile-style improvement sprint to test pre-staging and recipe readiness.
Days 31–60: Improve the constraint
- Pilot SMED on the highest-frequency changeover family.
- Standardise single-facer alignment and starch-viscosity checks.
- Trial order sequencing by width, flute and paper grade.
- Install visual FIFO lanes with maximum WIP limits.
- Use control charts for viscosity and key alignment measurements.
- Run a controlled comparison of changeover performance by shift and product family.
- Build the financial business case, including trim reduction, recovered capacity, avoided rework and inventory release. Use break-even analysis for any proposed equipment or automation investment.
Days 61–90: Lock in the future state
- Expand the best-performing changeover method across both shifts.
- Update standard work, training and escalation rules.
- Audit trim and defect performance against the target state.
- Review control-chart signals weekly.
- Confirm FPY and Rolled Throughput Yield, not only final dispatch yield.
- Complete a tollgate review and assign process ownership.
- Apply the Zero Defects principle associated with Philip Crosby: the standard is doing the work correctly the first time, supported by capable processes rather than final inspection alone.

Start building capability, not just another map
A VSM is valuable because it turns disconnected complaints (long changeovers, trim, defects, WIP and late dispatch) into one evidence-based improvement system.
For plant leaders, a Lean Six Sigma Green Belt provides the practical capability to lead this type of cross-functional project. For complex capacity, quality and governance challenges, Black Belt training develops the advanced statistical and leadership skills required to deliver sustainable results. A White Belt is an effective starting point for anyone who needs to understand DMAIC, waste and process improvement fundamentals.
Explore Lean Six Sigma Green Belt Online Training or develop advanced project leadership through Lean Six Sigma Black Belt Online Training. Lean 6 Sigma Hub courses are CSSC-accredited, self-paced and built around practical application, case studies and worked examples.
Start your Lean Six Sigma certification journey and learn how to convert a current-state map into measurable flow, quality and delivery improvement.
Kaizen. Kai-Care. Kai-Done. Lean Six Sigma.