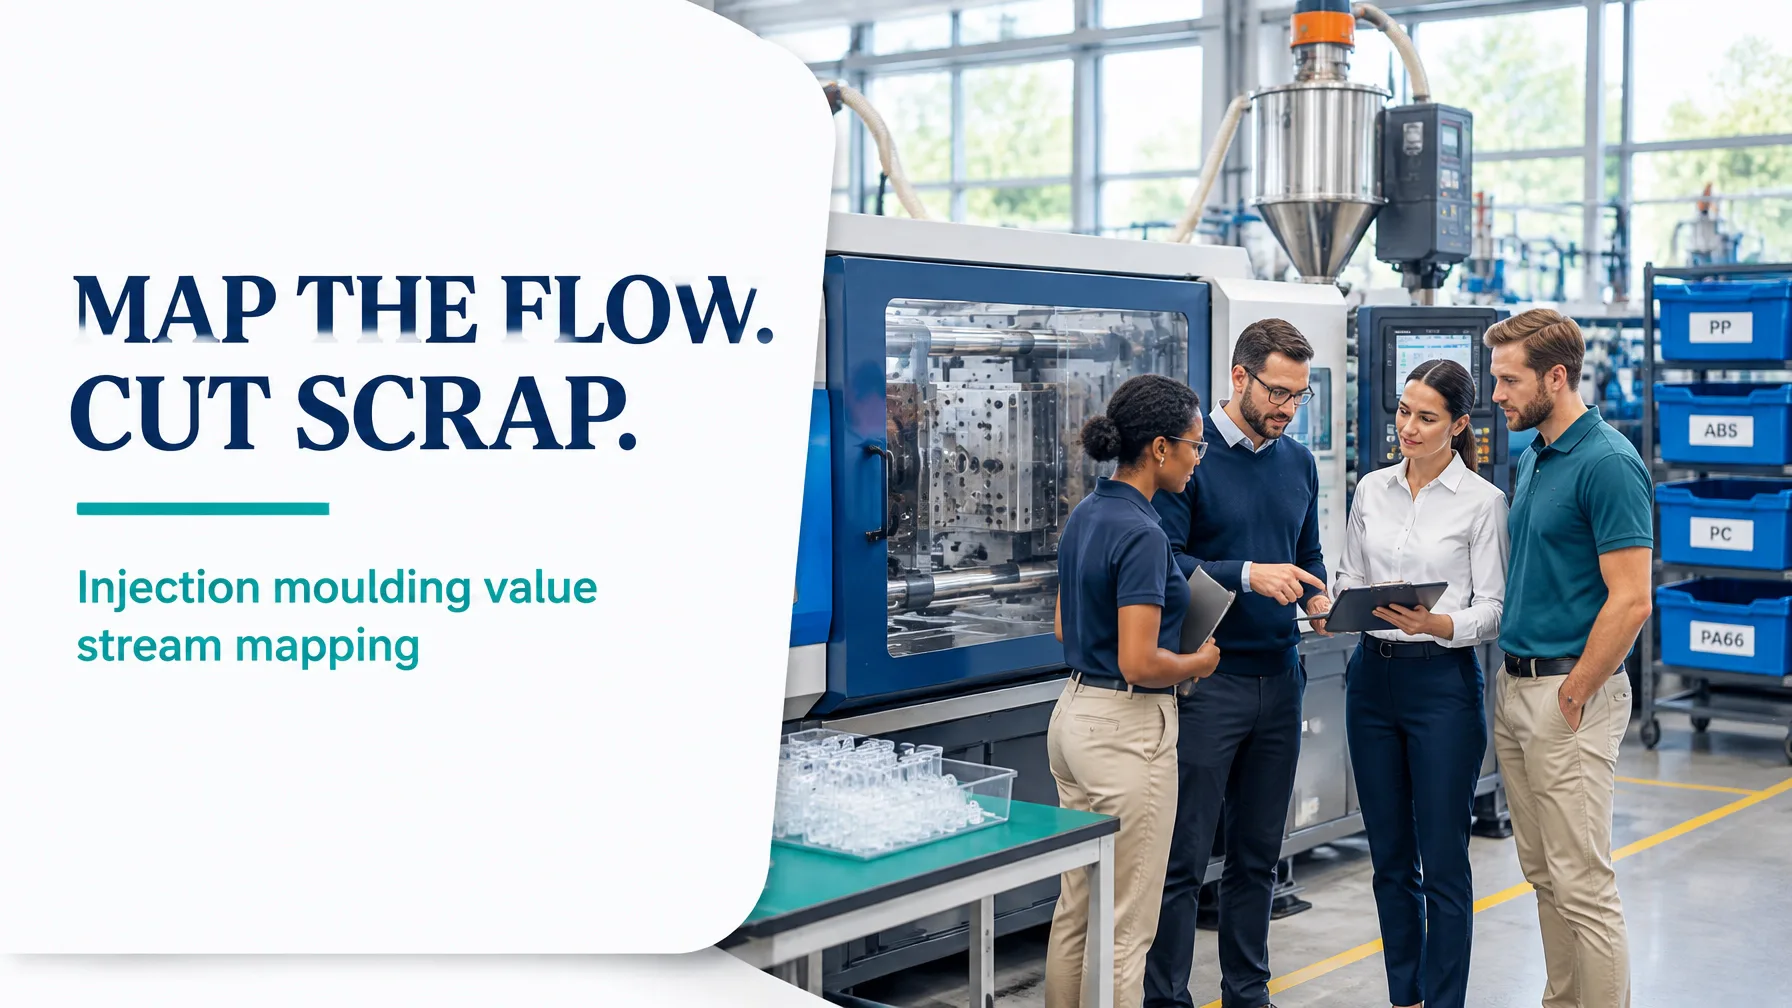
In injection moulding, the press cycle is only one part of the customer’s value stream. Resin may wait for drying, moulds may wait for preparation, finished parts may queue for inspection, and defects may travel through several operations before returning to the press as rework.
Value stream mapping makes this entire system visible. Rather than optimising one machine in isolation, the team can see how material, information, inventory, quality and time connect from resin preparation to customer dispatch. This is the practical purpose of VSM in Lean Six Sigma: identify the difference between value-added time, process time and elapsed lead time, then design a better flow.
This worked example follows a 24-cavity injection moulding cell producing a high-volume component with a small downstream assembly requirement.
1. Define the value stream boundary and customer value
The selected product family is a moulded component with similar resin, tooling, inspection and assembly requirements. It represents approximately 350,000 good parts of weekly customer demand and is suitable for a focused VSM workshop because it runs through the complete process family.
The boundary is:
Resin receiving and drying → material handling → mould changeover and set-up → injection cycle → cooling and part removal → degating → inspection → assembly → packing → warehousing → dispatch
The customer defines value as:
- A conforming part within dimensional and functional CTQs
- Correct assembly configuration
- Correct quantity and packaging
- On-time delivery
- Stable quality without unplanned sorting or rework
The cell operates three eight-hour shifts, five days per week, giving:
- Scheduled time: 3 × 8 × 5 = 120 hours
- Available seconds: 120 × 60 × 60 = 432,000 seconds per week
- Customer demand: 350,000 good parts per week
- Takt time: 432,000 ÷ 350,000 = 1.234 seconds per good part
The press has 24 cavities and an average injection cycle of 20 seconds, equivalent to:
20 ÷ 24 = 0.833 seconds per part
The cycle is faster than takt, but the margin is narrow once changeovers, downtime, defects and rework are included.
Lean Enterprise Institute’s explanation of value stream mapping provides a useful conceptual reference: the map should include both material and information flow, not only the visible production steps.
2. Current-state map: where time and capacity are lost
The information flow begins with a weekly customer forecast and purchase schedule. Planning converts this into a daily press schedule. The production supervisor releases work orders, while quality approval is required after each mould changeover before normal production resumes.
The current-state material flow is:
Resin drying → press queue → mould changeover → injection moulding → cooling and part removal → degating → inspection → assembly → packing → finished-goods warehouse → dispatch
| Process step | Current operating data |
|---|---|
| Resin drying | 240-minute drying cycle; 2,400 kg waiting; parameter variation contributes to moisture-related defects |
| Material handling to press | 6 minutes per lot; material is moved from a central area rather than a point-of-use supermarket |
| Mould changeover and set-up | 14 changeovers per week; average 95 minutes each, or 1,330 minutes weekly |
| Injection cycle | 20 seconds per shot; 24 cavities; 390,942 gross parts per week at the observed run time |
| Cooling and part removal | Included in the 20-second cycle; cooling variation contributes to dimensional instability |
| Degating | 0.7 seconds per part; queue of 6,000 parts |
| Inspection | 1.5 seconds per part; queue of 2,400 parts; first-pass yield is 93.8% |
| Assembly | 12 seconds per good part; queue of 3,600 parts |
| Packing | 0.8 seconds per part; 18,000 finished parts in storage |
| Warehousing and dispatch | Finished goods wait for shipment sequencing; on-time delivery is 91% |
After the 1,330 minutes of planned changeover time, the press has 352,200 seconds available for production. Observed uptime within that production window is 92.5%, giving:
- Actual running time: 352,200 × 92.5% = 325,785 seconds
- Gross output: 325,785 ÷ 20 × 24 = 390,942 parts
- First-pass good output: 390,942 × 93.8% = 366,704 parts
- Nonconforming first-pass output: 24,238 parts per week
The reported 6.2% scrap/nonconformance rate includes approximately 14,856 parts entering rework loops and 9,382 parts disposed of as material scrap.
Lead time, process time and PCE
For a representative shipment of 1,200 good parts, the current process time is:
- Resin drying: 240 minutes
- Material handling: 6 minutes
- Changeover allocation: 95 minutes
- Injection: 17.8 minutes for approximately 1,279 gross parts
- Degating: 15 minutes
- Inspection: 32 minutes
- Assembly: 240 minutes
- Packing: 16 minutes
- Dispatch administration: 10 minutes
Total process time: 671.8 minutes
Of this, injection and assembly provide the principal transformation:
- Injection value-added time: 17.8 minutes
- Assembly value-added time: 240 minutes
- Total value-added time: 257.8 minutes
Factory lead time is 3.8 days, or 5,472 minutes. Therefore:
Process Cycle Efficiency (PCE) = 257.8 ÷ 5,472 = 4.7%
The remaining 4,800 minutes are waiting, queueing, storage, movement, approval and scheduling delay.

3. The eight DOWNTIME wastes in this moulding cell
The current map makes the eight DOWNTIME wastes specific and measurable:
- Defects: 24,238 nonconforming first-pass parts each week create rework, inspection and material loss.
- Overproduction: 18,000 finished parts are stored, including approximately 6,000 not tied to the next dispatch sequence.
- Waiting: 4,800 minutes of the 5,472-minute lead time are non-value-added. The largest queues occur before the press, inspection and assembly.
- Non-utilisation of talent: Technicians spend 22.2 hours each week on the 14 long changeovers, with additional time spent manually recording data instead of improving settings and standard work.
- Transportation: Resin, moulds, work-in-process and finished goods travel approximately 84 kilometres per week through the facility.
- Inventory: The stream holds approximately 31,200 part-equivalents, plus 2,400 kg of resin waiting for production.
- Motion: Each changeover includes approximately 18 minutes of searching, walking and tool retrieval. Across 14 weekly changeovers, this is 252 minutes of avoidable motion.
- Extra processing: Full visual inspection consumes approximately 163 labour-hours per week at 1.5 seconds per part, while rework adds another processing loop without increasing customer value.
The bottleneck is not simply the moulding machine. It is the combined constraint created by changeover capacity, first-piece approval, quality variation and downstream queues.
4. Future-state design: flow, pull and built-in quality
The future-state map should not begin with an isolated target for the press. It should connect demand, takt, quality and capacity across the entire value stream.
Kaizen burst 1: stabilise resin and process inputs
Create a point-of-use resin supermarket with labelled material status, standard drying recipes and controlled dew-point checks. Reduce the drying cycle from 240 to 180 minutes by matching parameters to the resin specification and validating moisture results.
At the press, standardise barrel temperature, injection pressure, cooling time and mould-condition checks. Use control charts for the critical dimensions and establish an Andon signal for abnormal moisture, temperature or cavity pressure.
Kaizen burst 2: apply SMED to mould changeover
The current 95-minute changeover contains internal and external work. Pre-stage the next mould, clamps, resin, cooling connections, recipe and inspection documents while the press is running.
The target is a 9-minute average changeover:
- Confirm the next job and prepare the mould cart.
- Stage all tools, clamps and material externally.
- Use quick-connect services and standard clamp positions.
- Load the validated machine recipe.
- Run a first-piece check using a defined approval standard.
- Release the cell immediately when CTQs are confirmed.
Weekly changeover time falls from 1,330 minutes to 126 minutes, releasing 1,204 minutes, or approximately 20 hours, of scheduled capacity.
Kaizen burst 3: create pull between operations
Use a small supermarket between moulding, inspection and assembly. A kanban signal should replenish only what the downstream process consumes. A heijunka box can level the weekly schedule across the 14 changeovers rather than allowing large batches to build ahead of demand.
The future-state target is:
- Press-to-degate WIP: 6,000 to 1,200 parts
- Inspection queue: 2,400 to 600 parts
- Assembly queue: 3,600 to 1,200 parts
- Finished goods: 18,000 to 6,000 parts
Kaizen burst 4: move quality into the process
Replace delayed detection with in-process checks for cavity pressure, mould temperature, moisture, part weight and critical dimensions. Use first-piece approval as a rapid, digitally recorded checkpoint rather than a queue between production and quality.
Ci Flow can support this mapping work digitally through a connected value stream mapping workspace, allowing teams to record process evidence, lead time, inventory, performance and future-state actions in one project record. Ci Flow is a separate operational-excellence product from SigmaFlow and is designed for governed improvement projects, tool evidence and portfolio visibility.

5. Current state versus future state
| Metric | Current state | Future-state target |
|---|---|---|
| Factory lead time | 3.8 days / 5,472 min | 1.6 days / 2,304 min |
| Process time per 1,200-good-piece lot | 671.8 min | 489.6 min |
| Value-added time | 257.8 min | 256.2 min |
| PCE | 4.7% | 11.1% |
| Average changeover | 95 min | 9 min |
| Weekly changeover time | 1,330 min | 126 min |
| Scrap/nonconformance | 6.2% | 1.5% |
| OEE | 83.3% | 94.6% |
| Availability within run window | 92.5% | 96.0% |
| Scheduled-time utilisation | 75.4% | 94.3% |
| WIP | 31,200 part-equivalents plus resin | 9,600 part-equivalents plus 600 kg resin |
| On-time delivery | 91% | 98% |
Future OEE is calculated as:
96.0% availability × 100% performance × 98.5% quality = 94.6%
For the future-state lot, approximately 1,218 gross parts are required to produce 1,200 good parts at 1.5% nonconformance. The 19.2-second cycle produces the required output with substantial capacity available for planned demand rather than uncontrolled overproduction.
6. 30/60/90-day kaizen sequence

Days 0–30: establish control
Owner: Process Engineer
Support: Quality Engineer, Shift Supervisors
- Confirm the product family, takt and CTQs.
- Validate cycle-time, scrap and WIP data by shift.
- Complete a changeover observation sheet.
- Standardise resin drying parameters.
- Install visual WIP limits and defect categories.
- Establish daily review of availability, first-pass yield and on-time delivery.
Milestone: verified current-state map and baseline dataset.
Days 31–60: create flow
Owner: Production Manager
Support: Toolroom Lead, Materials Planner, Quality Engineer
- Pilot the SMED changeover on the 24-cavity press.
- Pre-stage moulds, tools and validated recipes.
- Introduce a supermarket and kanban signals.
- Launch heijunka-based weekly sequencing.
- Add in-process cavity pressure and dimensional checks.
- Reduce average changeover below 20 minutes.
Milestone: WIP below 18,000 part-equivalents and changeover below 20 minutes.
Days 61–90: sustain and govern
Owner: Plant Manager
Support: Continuous Improvement Lead, Finance Partner
- Confirm the 9-minute changeover target.
- Complete a capability review for CTQs.
- Audit standard work across all three shifts.
- Link the control plan to daily tier meetings.
- Review savings, capacity release and delivery performance.
- Replicate the future-state design across similar product families.
Milestone: 1.5% nonconformance, 98% on-time delivery and a documented control plan.
Build the capability to improve the whole stream
A well-executed VSM workshop gives process technicians, quality engineers and plant managers a common fact base. It also provides the structure for a broader Lean Six Sigma project: define customer value, measure the flow, analyse root causes, improve the system and control the gains.
To lead this work with stronger statistical, project and change-management capability, explore Lean 6 Sigma Hub’s CSSC-accredited Lean Six Sigma Green Belt training. Professionals leading complex, cross-functional transformations can progress to Lean Six Sigma Black Belt online training. You can also review the broader Lean Six Sigma certification pathway.
Start your Lean Six Sigma certification journey, map your injection moulding value stream, and turn released capacity into measurable customer value.
Kaizen. Kai-Care. Kai-Done. Lean Six Sigma