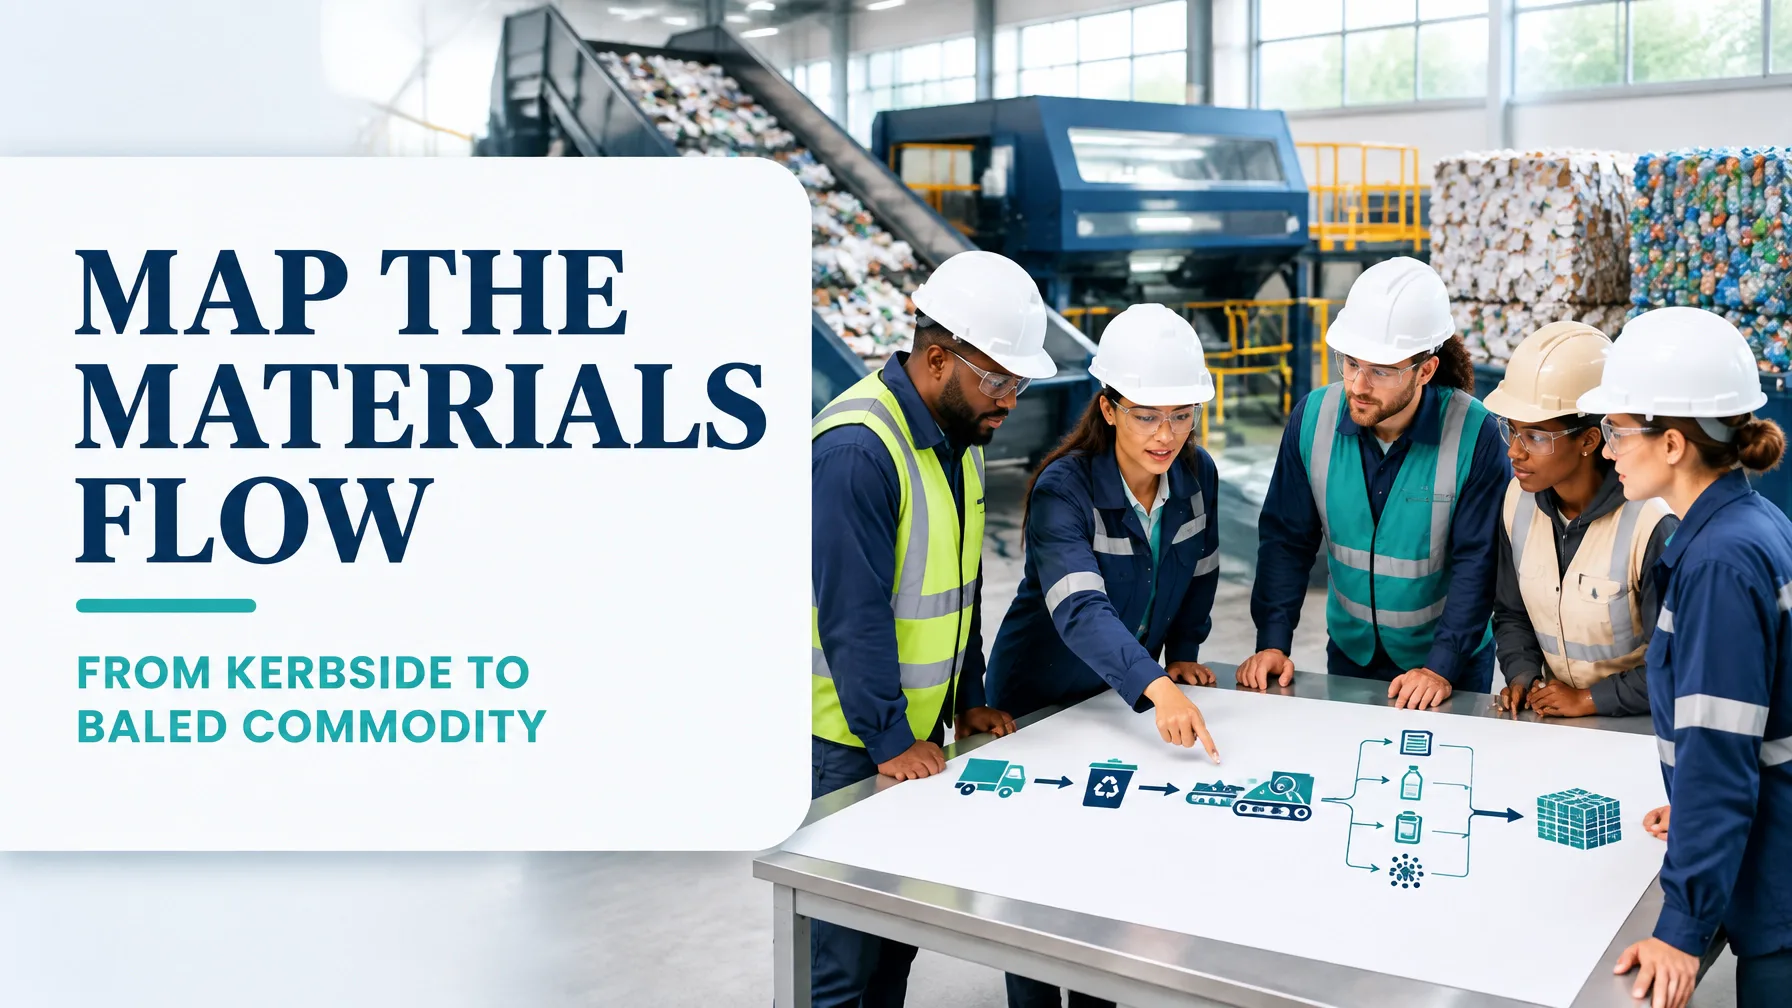
In a modern materials recovery facility (MRF), tonnes can move continuously while customer value remains trapped in queues, rework loops, contamination and poorly balanced equipment. Value Stream Mapping (VSM) makes that hidden performance visible.
VSM is a Lean method for documenting the sequence of activities, information flows, material flows and waiting time required to deliver an output. In recycling operations, the output is not simply “processed waste.” It is a set of saleable commodity streams (such as paper, cardboard, PET, HDPE and aluminium) produced to customer quality specifications.
The method is particularly valuable because it connects throughput, contamination, residuals, lead time, labour, equipment availability and bale quality on one view. The EPA Lean & Environment Toolkit also recommends extending conventional VSM with environmental data and a dedicated materials line.
This worked example uses a hypothetical but realistic MRF processing 240 tonnes per day across two shifts.
1. Select the Value Stream Boundaries
The first discipline is scope. A map that includes every collection route, municipal contract and downstream reprocessor can become too broad to manage. For this project, the value stream begins when a kerbside collection vehicle arrives at the facility and ends when compliant commodity bales are dispatched.
Scope definition
Start point: Kerbside collection vehicle receival and weighbridge verification.
Process sequence:
- Vehicle receival and weighing
- Tipping-floor unloading and temporary buffering
- Presort and removal of large contaminants
- Screening by size and material characteristics
- Optical sorting into commodity streams
- Manual quality control
- Contamination rework or residual disposal
- Baling and bale identification
- Commodity storage and dispatch
End point: Confirmed, saleable bales loaded for customer dispatch.
The map should also include the information flow: collection schedules, inbound contamination data, commodity specifications, dispatch orders, equipment alarms, quality holds and customer feedback.
For a practical workshop, assemble representatives from receival, tipping-floor operations, maintenance, sorting, quality, baling, logistics, sales and environmental compliance. A gemba walk is essential. The map must represent what actually happens, not what the standard operating procedure suggests should happen.

2. Current-State Map: Worked MRF Numbers
Assume the facility operates two eight-hour shifts and receives 240 tonnes per day, or approximately 120 tonnes per shift.
The customer demand rate is:
[
\text{Takt time} = \frac{16 \text{ available hours}}{240 \text{ tonnes}} = 0.0667 \text{ hours per tonne}
]
This equals 4 minutes per tonne, or a required average flow of 15 tonnes per hour.
The current state shows that the optical sorter is close to the demand rate. Its nameplate rate is 18 tonnes per hour, but 6% downtime reduces effective capacity:
[
18 \times 94% = 16.92 \text{ tonnes per hour}
]
That leaves only 1.92 tonnes per hour of effective capacity above takt demand, making the process vulnerable to minor stoppages, contamination spikes and changeover losses.
Current-state process data
| Process step | Observed rate or cycle time | Uptime / availability | Average WIP or queue |
|---|---|---|---|
| Receival and weighbridge | 18 min per truck | 98% / 96% | 8 tonnes |
| Tipping-floor unload | 12 min per truck | 96% / 94% | 26 tonnes |
| Presort | 42 t/hr; 1.4 min/t | 92% / 90% | 14 tonnes |
| Screening | 25 t/hr; 2.4 min/t | 91% / 89% | 12 tonnes |
| Optical sorting | 18 t/hr; 3.3 min/t | 94% / 88% | 12 tonnes |
| Manual quality control | 4.0 min/t of active inspection | 97% / 95% | 8 tonnes |
| Baling | 3.2 min/t of elapsed processing | 90% / 86% | 12 tonnes |
| Dispatch staging | 3 min/t handling time | 96% / 94% | 0–10 tonnes |
The facility has approximately 72 tonnes of average WIP across buffers and queues. The total elapsed lead time from receival to dispatch averages 4.8 hours, while cumulative value-added process time is only 71 minutes.
Process Cycle Efficiency (PCE) is therefore:
[
\text{PCE} = \frac{71}{288} \times 100 = 24.7%
]
In other words, only 24.7% of the elapsed time directly processes or verifies material. The remaining time is primarily waiting, buffering, transport, inspection delay or rework.
Material and quality performance
The current material balance is:
- 240 tonnes/day inbound
- 22% residual rate: 52.8 tonnes/day sent to landfill or another residual pathway
- 78% recovered material: 187.2 tonnes/day entering saleable or potentially saleable streams
- 14.5% inbound contamination
- 82.4% first-pass yield
- 4.6% contamination in finished commodity bales
- 14% of bales downgraded or held for additional inspection
The current-state map should show these flows explicitly. Contamination is not a side note; it is a branch in the material line that consumes labour, occupies equipment and reduces commodity value.
3. Identify the Eight Wastes in an MRF
The DOWNTIME acronym provides a structured way to examine the current state.
D, Defects
Contaminated bales, incorrect commodity classification, damaged packaging and wet fibre are defects. A bale containing 4.6% contamination may require rework, a price deduction or customer rejection.
O, Overproduction
Overproduction occurs when the facility creates bales before dispatch demand, grade confirmation or storage capacity exists. Excess baling can produce inventory that must be restacked, rehandled or regraded.
W, Waiting
Waiting appears when trucks queue at receival, material waits on the tipping floor, optical sorting pauses for maintenance, or bales wait for quality approval. The current map identifies 4.8 hours of total lead time against only 71 minutes of value-added work.
N, Non-utilisation of talent
Operators often know which routes generate the highest contamination and which alarms precede stoppages. If that knowledge is not captured through structured problem-solving, the facility loses practical expertise that could improve settings, standard work and training.
T, Transportation
Unnecessary movement occurs when tipped material is relocated multiple times, rejected bales travel back to quality control, or finished bales are moved between distant staging areas.
I, Inventory
WIP on the tipping floor, buffer piles before optical sorting and finished bales awaiting dispatch all represent inventory. The current 72 tonnes of average WIP conceals flow problems and increases handling exposure.
M, Motion
Operators may walk excessive distances to collect samples, clear chutes, retrieve labels or access tools. Poorly positioned inspection points increase fatigue and reduce available quality-control time.
E: Extra processing
Extra processing includes repeated manual sorting, re-baling, second inspections, relabelling and contamination removal that should have been prevented or contained earlier.

4. Build the Future State
The future-state map should not simply remove every buffer. Some controlled buffers protect the system from collection variability, planned maintenance and commodity changeovers. The goal is deliberate flow, not indiscriminate inventory reduction.
Establish flow around takt
With demand at 15 tonnes per hour, the optical sorting system should be managed to a stable operating target rather than pushed intermittently above capacity. A visual Andon signal can identify stoppages, contamination spikes and chute blockages in real time.
The future state should include:
- A controlled tipping-floor supermarket sized for a defined operating window
- FIFO lanes for inbound material by collection route or contamination profile
- A daily plan based on 15 t/hr demand flow
- Standard response times for equipment alarms
- A short escalation path from operator to maintenance and production leadership
Level-load the tipping floor
Collection arrivals are rarely uniform. Level loading can be achieved through appointment windows, route sequencing and designated buffer limits. For example, the facility may maintain a 20–25 tonne operating buffer rather than allowing the tipping floor to build beyond 40 tonnes.
The tipping-floor visual board should show:
- Planned arrivals by hour
- Actual tonnes received
- Contamination risk by route
- Available downstream capacity
- Maximum buffer limits
- Priority material requiring processing
Standardise commodity campaign changeovers
Changing optical sorter recipes, bunker assignments or bale specifications can create hidden downtime. A standard changeover sequence should define:
- Confirm the next commodity campaign
- Verify recipe, bunker and label settings
- Clear the previous material
- Run a controlled test sample
- Obtain quality confirmation
- Release the line to normal production
A target of reducing average changeover from 28 minutes to 15 minutes could recover more than four hours of productive capacity across a week of scheduled campaigns.
Contain contamination at the kerbside
The most effective contamination is prevented or identified before it enters the main process. Create a route-level containment loop:
- Record contamination by truck, route and collection day
- Photograph or classify the top contaminant categories
- Provide feedback to collection contractors or councils
- Isolate high-risk loads for controlled tipping
- Add targeted presort staffing during known contamination peaks
- Track whether corrective action reduces contamination over the following four weeks
The target future state is to reduce inbound contamination from 14.5% to 9%, finished-bale contamination from 4.6% to 2.8%, and residuals from 22% to 17%.
5. Current State Versus Future State
| Metric | Current state | Future state target |
|---|---|---|
| Average lead time | 4.8 hours | 2.6 hours |
| Value-added process time | 71 minutes | 62 minutes |
| Process Cycle Efficiency | 24.7% | 39.7% |
| Daily throughput | 240 tonnes | 255 tonnes |
| Residual rate | 22% | 17% |
| Finished-bale contamination | 4.6% | 2.8% |
| Bales downgraded or held | 14% | 6% |
| Cost per tonne processed | $118 | $102 |
| Average WIP | 72 tonnes | 42 tonnes |
| Recordable safety incidents per quarter | 3 | 1 or fewer |
These are improvement targets, not guaranteed results. The facility should validate them through a controlled pilot, measurement-system checks and daily management.
6. A 90-Day Kaizen Sequence
Days 1–30: Stabilise and measure
Owners: Operations Manager, Quality Lead and Maintenance Supervisor.
Actions:
- Confirm the current-state data at each process step
- Audit contamination by route and collection day
- Establish WIP limits and visual buffer controls
- Create an optical sorter downtime Pareto
- Standardise the quality definition for a saleable bale
Expected impact: Reduce unplanned waiting, improve baseline accuracy and identify the largest contributors to residuals and downgraded bales.
Days 31–60: Improve flow and containment
Owners: Production Manager, Collection Coordinator and Engineering Lead.
Actions:
- Pilot level-loaded tipping-floor schedules
- Introduce FIFO lanes and maximum buffer limits
- Run a contamination containment trial for the three highest-risk routes
- Standardise commodity campaign changeovers
- Trial Andon escalation for stoppages exceeding five minutes
Expected impact: Reduce WIP by 20–30%, improve effective optical-sorting availability and reduce repeat contamination handling.
Days 61–90: Control and scale
Owners: Site Manager, Finance Business Partner and Continuous Improvement Lead.
Actions:
- Validate the future-state metrics against the baseline
- Implement daily control charts for throughput, residual rate and bale contamination
- Link operator standard work to quality and safety checks
- Review cost per tonne and recovered commodity revenue
- Replicate successful controls across shifts and material campaigns
Expected impact: Move toward 255 tonnes per day, 17% residuals, 6% downgraded bales and a cost reduction of approximately $16 per tonne.
Turn MRF Data into Practical Improvement Capability
Value Stream Mapping gives MRF leaders a disciplined way to connect material recovery with customer value, environmental performance, operating cost and workforce safety. It also provides the foundation for the DMAIC method: define the contamination and flow problem, measure the current state, analyse root causes, improve the system and control the gains.
If you want to lead projects of this complexity, Lean 6 Sigma Hub’s CSSC-accredited Green Belt training develops practical capability in process mapping, data collection, root-cause analysis, statistical tools, control plans and project leadership. You can also use the Process Cycle Efficiency Calculator to quantify the gap between value-added work and total lead time.
Enrol in Lean Six Sigma certification training today and build the skills to improve throughput, protect material value and lead measurable operational change.
Kaizen. Kai-Care. Kai-Done. Lean Six Sigma