
In aluminium extrusion, customer value is created when the right profile reaches the customer in specification, on time, and with the required surface finish. Yet the total lead time is often governed less by the seconds spent shaping aluminium and more by queues, batch constraints, die changeovers, furnace loading, rework, and dispatch staging.
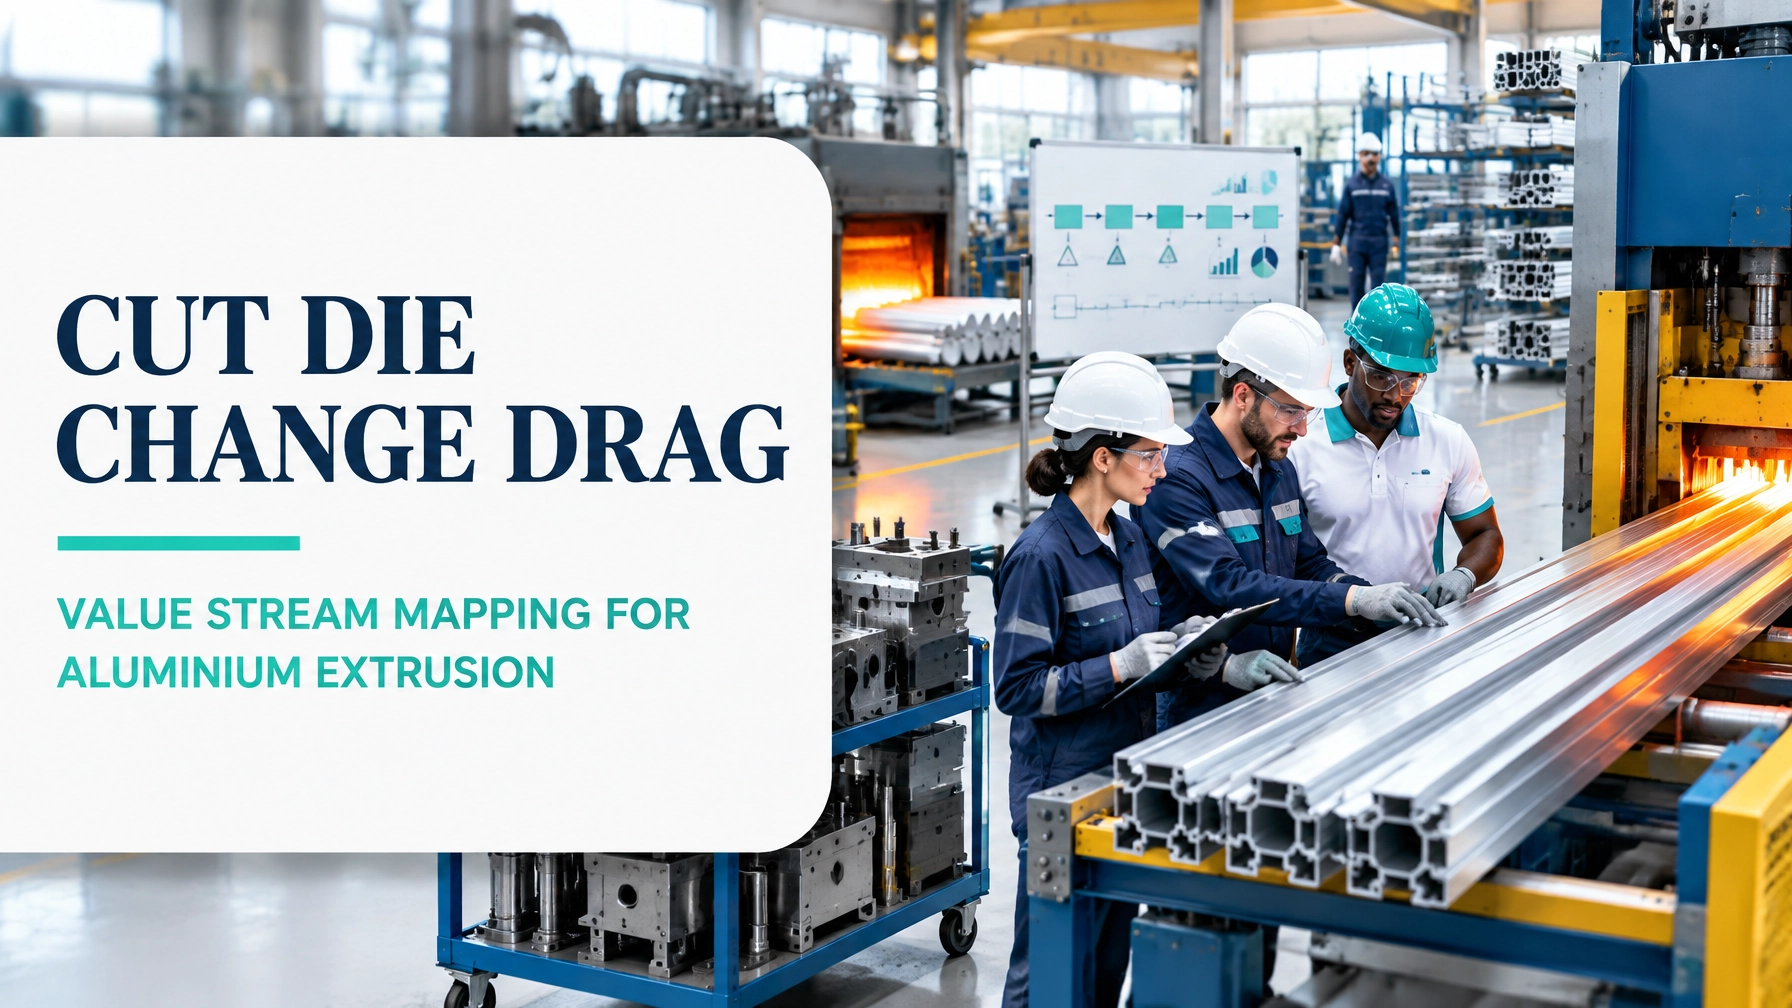
This deep-guide case study maps an aluminium extrusion value stream from billet sawing through anodised dispatch. The billet casting process is deliberately excluded so the team can focus on the controllable flow across billet preparation, extrusion, ageing, anodising, packing, and dispatch.
The objective is clear: reduce order-to-dispatch lead time from 6.5 days to 2.8 days, improve OEE from 61% to 78%, and remove the die change delays that interrupt flow.
1. Define the Value Stream Scope
The product family includes finished aluminium profiles that follow this route:
Billet saw and preheat → extrusion press → quench and cooling → stretch and cut → ageing → anodising → packing → dispatch
The scope begins when billets are released to the saw and ends when finished anodised profiles are staged for shipment. It excludes billet casting, customer order acquisition, and external transport after dispatch.
The plant serves demand of 138,000 kg of extruded profile per day across three presses. Available production time is:
- Two shifts × 11.5 hours
- 1,380 available minutes per day
- Demand rate: 138,000 kg ÷ 1,380 minutes = 100 kg per minute
- Takt time: 0.6 seconds per kilogram
This takt calculation sets the required customer rhythm. It does not mean one billet must be processed in 0.6 seconds; rather, the combined value stream must release finished profile at the equivalent demand rate.
For a practical VSM workshop, include representatives from:
- Press operations and die preparation
- Billet preparation and furnace operations
- Quality and metallurgy
- Ageing and anodising
- Maintenance and TPM
- Planning, logistics, packing, and dispatch
- Customer service or commercial operations
Value Stream Mapping should be treated as a cross-functional operating model, not merely a process drawing.
2. Current-State Map: Where Time Is Being Consumed

The current-state map captures both material flow and information flow. Production scheduling releases work to the presses, while downstream teams respond to batch availability, furnace capacity, anodising loads, and dispatch priorities.
Current-state process data
| Process step | Current operating condition |
|---|---|
| Billet saw and preheat | 25 minutes per batch of 12 billets |
| Press extrusion cycle | 92 seconds per billet |
| Die changeover | 45 minutes; 3.4 changeovers per shift |
| Die changes exceeding standard | 18% |
| Quench and cooling | 8 minutes |
| Stretch and cut to length | 100 seconds |
| Ageing oven | 8-hour batch cycle; 71% loading |
| Anodising | 96 minutes per load |
| Anodising colour mismatch rework | 2.7% |
| Packing | 14 minutes per stillage |
| Dispatch staging | 3.6 hours |
| Total order-to-dispatch lead time | 6.5 days |
| Value-added press and process time | 42 minutes |
| Rolled throughput yield | 88.4% |
| Overall equipment effectiveness | 61% |
| OEE availability | 74% |
| OEE performance | 88% |
| OEE quality | 94% |
| Press scrap | 4.8% |
The first important observation is the difference between 42 minutes of value-added process time and 6.5 days of total lead time. The customer is waiting for far longer than the aluminium is being transformed.
The second observation is the effect of die changes. At 45 minutes per changeover and 3.4 changeovers per shift, the press system spends approximately 153 minutes per shift in planned die-change activity before accounting for the 18% of changes that exceed the standard.
The third observation is batch imbalance. An ageing cycle of eight hours operating at only 71% loading creates a difficult combination: long thermal residence time and incomplete use of available capacity. This encourages larger queues before the oven and makes downstream anodising scheduling less responsive.
A simplified current-state flow is:
Billet batch → 25-minute saw/preheat cycle → press queue → 92-second billet cycle → die-change interruption → 8-minute cooling → 100-second stretch/cut → ageing queue and 8-hour batch → anodising queue → 96-minute load → packing queue → 3.6-hour dispatch staging
3. Identify the Eight DOWNTIME Wastes
The DOWNTIME framework provides a disciplined way to examine the map:
- Defects – Press scrap of 4.8% and anodising colour mismatch rework of 2.7% reduce effective output and consume capacity.
- Overproduction – Large press or ageing batches can produce profiles before anodising or dispatch capacity is ready.
- Waiting – Profiles wait for die availability, ageing capacity, anodising loads, packing space, and dispatch release.
- Non-utilised talent – Operators may spend time locating dies, checking schedules, or escalating avoidable stoppages instead of improving the process.
- Transportation – Multiple movements between press, ageing, anodising, packing, and staging increase handling and damage exposure.
- Inventory – Work in process accumulates between batch-driven steps, particularly before ageing and anodising.
- Motion – Unnecessary walking for tools, dies, quality records, and material identification extends changeover and handling time.
- Extra-processing – Re-inspection, colour rework, repeated paperwork, and correction of incomplete production information consume effort without increasing customer value.
The map should distinguish value-added time, necessary but non-value-added time, and avoidable delay. Furnace residence may be technically necessary, but waiting for a partially filled batch is a separate improvement opportunity.
4. Build the Future-State Value Stream

The future state should not simply demand faster work from operators. It should redesign the flow around customer demand, process capability, and constraint management.
Apply SMED to die changeover
The first priority is a press-focused SMED kaizen that reduces die changeover from 45 minutes to 12 minutes.
The team should:
- Separate internal tasks from external preparation.
- Preheat, clean, inspect, and stage the next die while the press is running.
- Create a complete die kit with tools, fasteners, checksheets, and identification.
- Use standard locations and visual controls for dies and changeover equipment.
- Record every changeover with a video or time observation sheet.
- Convert avoidable internal work into external setup activity.
- Establish a confirmation checklist before the press stops.
The 12-minute target should be supported by repeatable standard work, not by informal operator effort.
Balance the press line to takt
Press scheduling should be balanced to the 0.6-second-per-kilogram demand rhythm, while recognising billet geometry, alloy, profile complexity, and press capability.
A pull-based billet delivery system can release the next billet family based on a downstream signal rather than pushing large quantities into the press area. This reduces excess billet WIP and helps align billet preparation with actual press consumption.
Introduce kanban between press, ageing, and anodising
A controlled kanban loop should connect:
- Press output to ageing
- Ageing release to anodising
- Anodising completion to packing
Kanban quantities should be based on demand, replenishment time, batch constraints, and a defined safety allowance. The purpose is not to eliminate every buffer. It is to make each buffer visible, limited, and intentional.
Ageing oven loading should increase from 71% to above 92% through better family scheduling, recipe discipline, and pull-based release. The team must ensure that higher loading does not create excessive waiting or compromise metallurgical requirements.
Use TPM to improve anodising availability
Total Productive Maintenance should focus on the anodising line’s chronic losses:
- Planned cleaning and inspection of tanks, pumps, rectifiers, and handling systems
- Condition checks for temperature, chemistry, conductivity, and current density
- Autonomous maintenance standards for operators
- Pareto analysis of stops and colour mismatch rework
- First-response standards for abnormal conditions
Improving anodising availability and reducing colour mismatch will protect both OEE quality and downstream dispatch reliability.
5. Current State Versus Future State
The WIP figures below are expressed as flow-equivalent WIP at daily demand using Little’s Law. Current equivalent WIP is 6.5 days × 138,000 kg, or 897,000 kg. The future equivalent is 2.8 days × 138,000 kg, or 386,400 kg. The physical WIP count should be validated during the plant walk.
| Metric | Current state | Future-state target |
|---|---|---|
| Order-to-dispatch lead time | 6.5 days | 2.8 days |
| Value-added process time | 42 minutes | 42 minutes, controlled |
| OEE | 61% | 78% |
| Availability | 74% | 88% |
| Performance | 88% | 91% |
| Quality | 94% | 97% |
| Die changeover time | 45 minutes | 12 minutes |
| Press scrap | 4.8% | 2.1% |
| Rolled throughput yield | 88.4% | Above 95% |
| WIP, flow-equivalent | 897,000 kg | 386,400 kg |
The unchanged value-added process time is intentional. A strong Lean intervention does not automatically compress technically required processing. It removes waiting, setup loss, rework, and excess inventory around that processing.
6. Ninety-Day Kaizen Sequencing

Days 1–30: Stabilise the constraint
- Run the SMED die changeover kaizen.
- Capture current changeover elements and move preparation externally.
- Create die kits, standard locations, and a 12-minute pilot standard.
- Launch an hour-by-hour press performance board.
- Establish daily tiered huddles covering safety, quality, delivery, cost, and people.
- Confirm baseline data for scrap, RTY, changeover, and OEE.
Days 31–60: Connect the value stream
- Balance press production to demand and profile family requirements.
- Introduce pull-based billet delivery.
- Pilot kanban between press, ageing, and anodising.
- Raise ageing oven loading toward 92% or higher without violating process recipes.
- Begin TPM actions on the anodising line.
- Review WIP limits at every supermarket or staging point.
Days 61–90: Sustain and control
- Standardise the improved changeover method across all three presses.
- Complete anodising TPM checks and review availability trends.
- Link the hour-by-hour board to daily tiered accountability.
- Audit standard work, kanban signals, oven loading, and colour controls.
- Recalculate the current-state map and publish the future-state performance gap.
- Add control plans for die changeover, ageing release, anodising chemistry, and dispatch staging.
7. Link VSM to DMAIC and Digital Kaizen Execution
Value Stream Mapping provides the Lean structure; DMAIC provides the analytical discipline.
- Define: Establish the product family, customer demand, scope, business case, and CTQs.
- Measure: Capture cycle time, changeover, WIP, scrap, rework, OEE, loading, and dispatch delay.
- Analyse: Use Pareto charts, process capability, time observation, queue analysis, and root-cause methods.
- Improve: Implement SMED, pull, kanban, TPM, standard work, and line balancing.
- Control: Sustain gains with control plans, tiered huddles, visual boards, and verified process audits.
A digital platform such as the SigmaFlow Value Stream Mapping workspace can support current- and future-state mapping, while its Kaizen-oriented workspaces help connect improvement actions, ownership, documentation, and follow-through. The advantage is traceability: the map, the data, the action plan, and the control method remain connected.
For professionals seeking deeper capability, Lean Six Sigma online training provides a structured path from foundational principles to advanced project leadership. A CSSC-accredited certification helps practitioners apply tools such as VSM, OEE, SMED, TPM, DMAIC, and statistical analysis with greater confidence.
Start your Lean Six Sigma certification journey and learn to turn value stream data into measurable flow, capacity, and customer value.
Kaizen. Kai-Care. Kai-Done. Lean Six Sigma.