
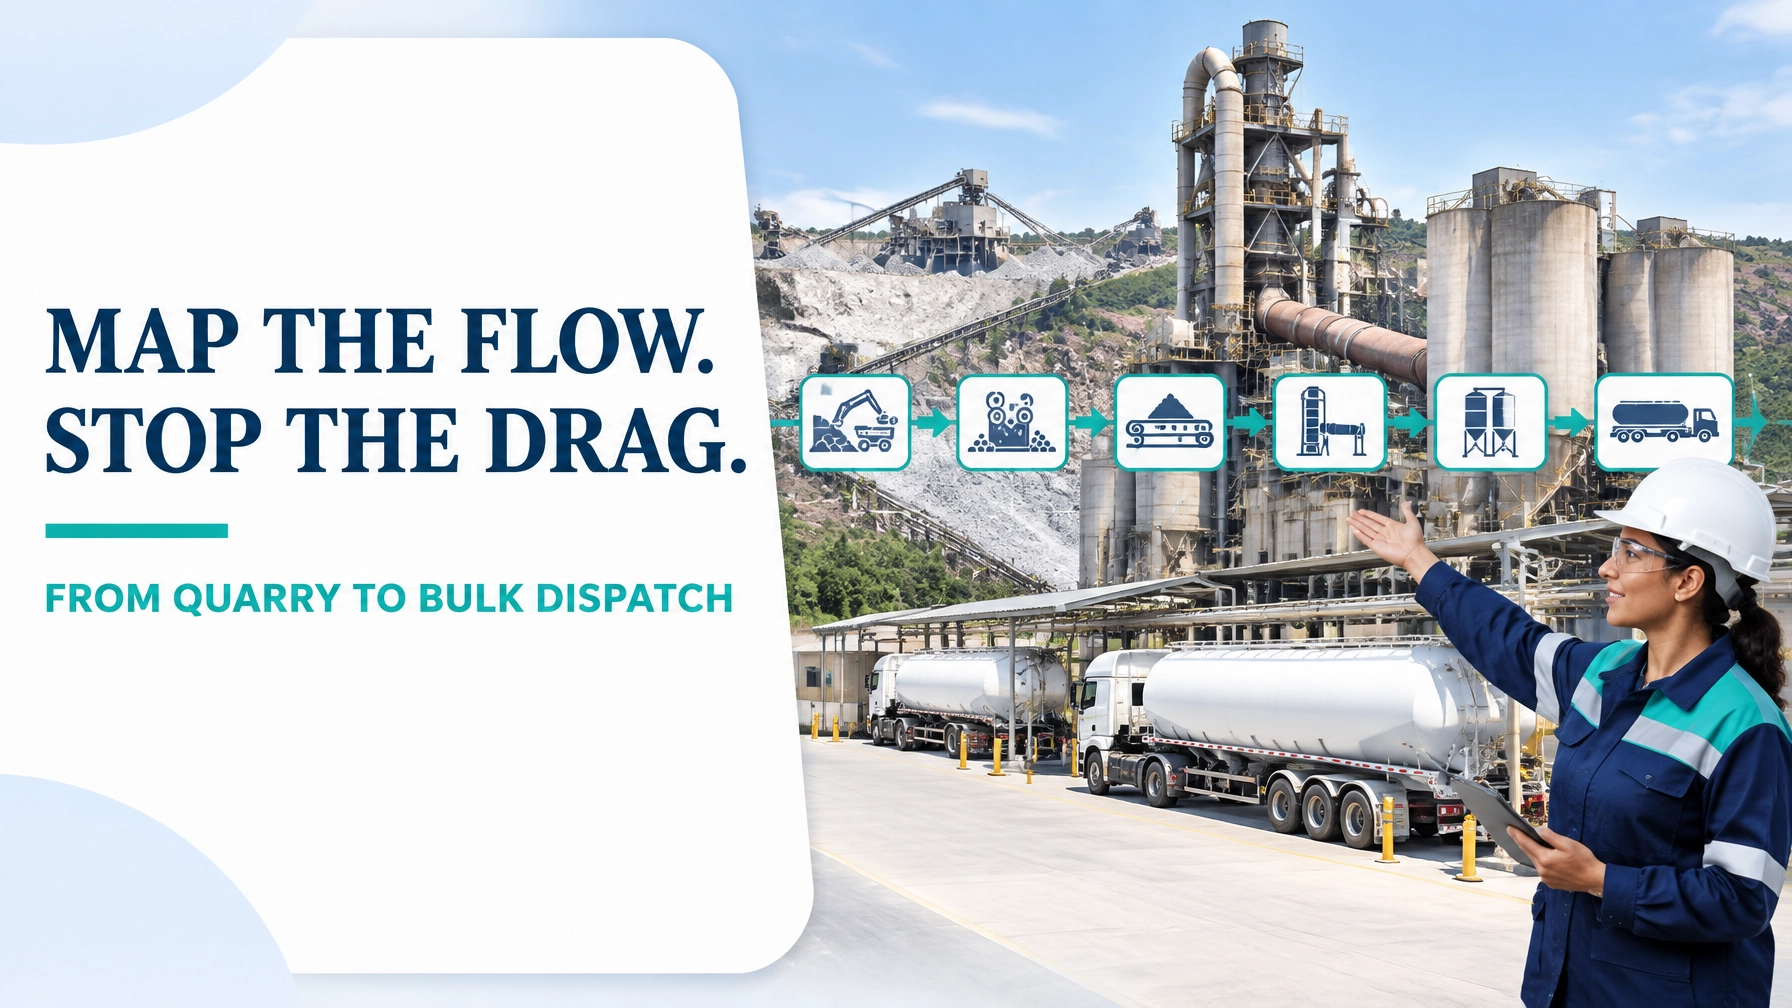
In heavy process manufacturing, value stream mapping is more than a flowchart. It is a fact-based view of how material, information, inventory and decisions move through the operation. For a cement plant, that means following the value stream from quarry feed and crushing through raw meal preparation, kiln and clinkerisation, cement grinding, silo storage and bulk tanker dispatch.
The objective is not to make the kiln behave like a discrete assembly line. The objective is to expose the delays, buffers, interruptions and information gaps surrounding the continuous process, and then design a more reliable flow.
The worked example below uses illustrative plant data to demonstrate the method. It is informed by published cement VSM research, including a case study that reported 76 hours of total lead time and 41 hours of value-added time across a cement production flow.1
1. Scope selection: define one product family and clear boundaries
A useful VSM begins with disciplined scope selection. If every cement grade, customer segment and dispatch route is included, the map becomes too broad to manage.
For this example, select:
- Product family: Ordinary Portland Cement (OPC), bulk dispatch
- Start boundary: Limestone and corrective-material feed from the quarry
- End boundary: Bulk cement loaded into customer tankers
- Included processes: Quarry/crushing, raw meal preparation, kiln and cooler, clinker storage, cement grinding, cement silo release and bulk loading
- Included information flow: Customer orders, production planning, laboratory release, maintenance notifications and truck scheduling
This boundary captures the principal material and information flow without mixing in bagged cement or unrelated product recipes.
2. Current-state map: make the kiln stop drag visible
The current-state map should be built through a gemba walk, production records, control-system data, laboratory logs and direct time observation. Record cycle time, uptime, changeover, WIP, queues, inventory days and quality losses at every major step.

Worked current-state data
The following example represents a plant producing approximately 48,000 tonnes of bulk OPC per month.
| Process | Cycle time | Uptime | WIP or queue | Changeover / interruption |
|---|---|---|---|---|
| Quarry and crushing | 8 h campaign | 82% | 18,000 t limestone | 2 h crusher setup |
| Raw meal grinding | 6 h batch | 88% | 7,200 t raw meal | 90 min recipe change |
| Kiln and clinkerisation | 24 h continuous window | 79% | 22,000 t clinker | 6 h average recovery after stop |
| Cement grinding | 8 h batch | 84% | 16,000 t cement | 3 h product changeover |
| Bulk packing and dispatch | 6 h daily operating window | 91% | 18-truck queue | 45 min loading-system reset |
The observed lead-time bridge is:
| Process | Lead time | Value-added time |
|---|---|---|
| Quarry and crushing | 12 h | 4 h |
| Raw meal grinding | 10 h | 5 h |
| Kiln and clinkerisation | 36 h | 22 h |
| Cement grinding | 10 h | 7 h |
| Bulk dispatch | 8 h | 3 h |
| Total | 76 h | 41 h |
The current Process Cycle Efficiency (PCE) is:
[
PCE = \frac{41}{76} \times 100 = 53.9%
]
That means only 53.9% of the elapsed time is classified as value-added in this illustrative stream. The remaining time is consumed by inventory, waiting, transportation, quality release, equipment recovery and other non-value-added activity.
The map should also display information timing. In this example, the quarry and kiln teams receive a daily production schedule, while dispatch changes customer priorities several times during the shift. That creates a familiar pattern: upstream teams produce for forecast, while downstream teams respond to actual demand.
3. The eight DOWNTIME wastes in cement manufacturing
The eight wastes, often remembered as DOWNTIME, must be translated into plant-specific observations.
Defects
Examples include off-spec clinker chemistry, incorrect cement fineness, failed laboratory release, misloaded tankers and rejected customer loads. A current-state baseline might show 3.6% of finished tonnes requiring re-blending, regrinding or downgrade disposition.
Overproduction
When the kiln runs ahead of cement demand, clinker stockpiles rise. Producing clinker without a controlled downstream requirement creates storage cost, handling and quality exposure. The 22,000-tonne clinker buffer in this example is a visible signal of disconnected flow.
Waiting
Waiting appears when kiln feed is interrupted, laboratory results are late, silo space is unavailable, maintenance clearance is pending or tankers queue at the weighbridge. The dispatch queue of 18 trucks is not simply a transport issue; it is a customer lead-time problem.
Non-utilisation of talent
Operators often know why kiln stops repeat, why samples are delayed or why truck documents are reworked. If improvement ideas remain informal and are not converted into standard work, the plant loses practical expertise. Include operator observations in the map and assign owners to verified countermeasures.
Transportation
Long haulage routes for limestone, raw meal, clinker and additives increase fuel use, handling and exposure to spillage. VSM should show both physical distance and the number of handling events.
Inventory
Track inventory as both tonnes and days of supply:
- Limestone stockpile: 12 days
- Raw meal silo: 1.8 days
- Clinker silo: 2.2 days
- Cement silo: 1.7 days
Inventory can protect a continuous process, but unexplained or excessive inventory conceals instability and increases working capital.
Motion
Operators may walk between control rooms, sampling points, weighbridges and laboratories multiple times per shift. A time observation sheet can quantify these routes. If a quality technician spends 110 minutes per shift walking and waiting for sample access, the map should treat that as improvement data, not anecdotal frustration.
Excess processing
Double grinding, unnecessary over-blending, excessive fineness and repeated sampling are common examples. The customer may not pay for cement ground beyond the required specification, but the plant pays through energy, wear and capacity consumption.
4. Future-state design: connect takt, pull and level loading
For 48,000 tonnes per month, assume 720 available production hours and 1,600 bulk tanker loads at 30 tonnes each.
The monthly dispatch takt is:
[
Takt = \frac{720 \text{ hours}}{1,600 \text{ loads}} = 0.45 \text{ hours/load}
]
That equals 27 minutes per tanker load. If the current average truck turnaround is 52 minutes, dispatch is not aligned with demand rhythm.

A practical future state should include:
- Pull from dispatch: Customer orders trigger a controlled cement-silo replenishment signal.
- Supermarket buffers: Establish minimum and maximum clinker and cement inventory rather than allowing stockpiles to expand without limits.
- Level loading: Smooth the daily mix of OPC orders across the planning horizon instead of releasing large batches followed by idle periods.
- Kiln reliability focus: Use stoppage Pareto analysis, preventive maintenance and rapid recovery standards to raise kiln uptime.
- Synchronized laboratory release: Define a sample-to-result service level and visual escalation when the limit is exceeded.
- Truck appointment scheduling: Match loading capacity to the 27-minute takt and separate documentation from loading wherever possible.
The future state does not eliminate every buffer. It makes each buffer intentional, visible and governed.
5. Current versus future performance targets
| Metric | Current state | 90-day target | Improvement logic |
|---|---|---|---|
| Total lead time | 76 h | 42 h | Reduce waiting, queue and uncontrolled inventory |
| Value-added time | 41 h | 31 h | Remove double processing and rework |
| PCE | 53.9% | 73.8% | Improve flow without adding unnecessary capacity |
| Kiln uptime | 79% | 86% | Address repeat stoppage causes |
| Clinker WIP | 22,000 t | 12,000 t | Introduce min/max supermarket controls |
| Cement inventory | 16,000 t | 10,000 t | Level production to dispatch demand |
| Off-spec/rework rate | 3.6% | 1.5% | Strengthen process control and release discipline |
| Truck turnaround | 52 min | 31 min | Appointment scheduling and standard loading work |
| Kiln-feed interruptions | 9 per week | 3 per week | Stabilise raw meal replenishment and escalation |
These targets should be validated against plant capacity, safety requirements, maintenance strategy and customer service obligations before implementation.
6. A 90-day kaizen sequence

Days 1–30: establish control
Owner: VSM leader and production manager
- Confirm product family and map boundaries.
- Validate current-state data at the quarry, kiln, grinding and dispatch points.
- Create a downtime Pareto for kiln and raw meal interruptions.
- Introduce truck appointment slots and a dispatch queue board.
- Target: 100% daily visibility of WIP, queues and equipment interruptions.
Days 31–60: stabilise the constraint
Owner: Kiln manager and maintenance manager
- Standardise first response to kiln stoppages.
- Launch a focused reliability sprint on the top three recurring stop causes.
- Set raw meal and clinker supermarket limits.
- Define laboratory sample-to-result escalation rules.
- Target: kiln uptime of 84%, clinker WIP below 15,000 tonnes and truck turnaround below 40 minutes.
Days 61–90: connect the future-state flow
Owner: Operations excellence manager and supply-chain manager
- Level-load OPC production against dispatch demand.
- Reduce cement mill changeover through internal/external activity separation.
- Remove verified double-grinding and over-blending causes.
- Audit standard work and publish a control plan.
- Target: 76-hour lead time reduced to 42 hours, PCE above 70% and off-spec rate below 1.5%.
The Analyse Phase should continue throughout the sequence. Use stratification, Pareto analysis, control charts and cause-and-effect analysis to distinguish common-cause variation from special causes. Do not reduce inventory or add pull signals until the process is stable enough to respond reliably.
Build capability to lead the improvement
A cement VSM is valuable only when the team can interpret the map, test root causes and convert future-state design into sustained operating discipline. That requires practical Lean Six Sigma capability across production, maintenance, quality, logistics and leadership.
Lean 6 Sigma Hub offers CSSC-accredited, self-paced online certification from White Belt through Master Black Belt, with practical case studies, worked examples, charts, templates and end-to-end DMAIC application. Explore the Lean Six Sigma online training or develop project leadership capability through the Lean Six Sigma Green Belt course.
Start your Lean Six Sigma certification journey today and learn to turn value stream data into measurable operational results.
Kaizen. Kai-Care. Kai-Done. Lean Six Sigma